In the modern industrial landscape, the efficiency of waste processing hinges on the precision of cutting tools. Maintaining a high-performance shredding system requires a strategic approach to chipper shredder blade replacement to ensure that materials are processed without interruption. When blades dull or chip, the energy consumption of the machinery rises, and the quality of the output diminishes, making timely maintenance a global operational priority.
Across various sectors, from paper recycling to industrial waste management, the demand for durable cutting edges is constant. The technical challenge lies in balancing the hardness of the material with its impact resistance to avoid premature failure. A systematic chipper shredder blade replacement schedule not only prevents costly unplanned downtime but also optimizes the throughput of raw materials, directly affecting the bottom line of recycling facilities.
Understanding the nuances of material selection—such as choosing between alloy tool steel and cemented carbide—is essential for maximizing equipment longevity. By prioritizing a high-quality chipper shredder blade replacement, operators can achieve higher purity in recycled pulp and reduce the overall carbon footprint of their manufacturing process through improved energy efficiency.
Material Science in Blade Selection
The foundation of an effective chipper shredder blade replacement strategy lies in selecting the correct metallurgy for the specific waste stream. For instance, 9CrSi alloy tool steel offers a cost-effective solution for ordinary office paper due to its high hardness, while Cold Working Die Steel (Cr12MoV/SKD-11) provides the necessary balance of wear and impact resistance for tougher materials like cardboard and laminated papers.
For extreme environments involving metal foil composite papers or insulation materials, cemented carbide (Tungsten Carbide) is the gold standard, boasting hardness levels of HRA89 or above. This material significantly reduces the frequency of replacement and supports continuous high-intensity operations, ensuring that the shredding process remains efficient even when facing the most abrasive materials.
Structural Adaptations for Different Scenarios
Different shredding requirements demand specific blade geometries to optimize the cutting action. Straight knives are ideal for low-confidentiality office documents, offering a simple and low-cost installation. However, when dealing with high-toughness cardboard or laminated paper, sawtooth knives are preferred because their serrations reduce cutting resistance and make information recovery significantly more difficult.
For large-scale industrial waste paper processing, spiral blades are employed to facilitate progressive crushing, which reduces the motor load and increases overall throughput. This design allows for a continuous flow of material, preventing the "slugging" effect often seen with straight blades in high-volume environments.
In cases involving multi-layer corrugated cardboard or hard boxes, multi-axis claw knives (ranging from 3 to 12 claws) are utilized. Their staggered arrangement provides superior impact resistance and the ability to grip and tear large volume materials, ensuring that the material is properly sized before it reaches the finer grinding stages.
Core Benefits of Precision Maintenance
Implementing a rigorous chipper shredder blade replacement protocol leads to immediate improvements in energy efficiency. When blades are sharp, the motor requires less torque to shear through tough fibers, which can reduce energy costs by up to 25% when combined with frequency conversion speed regulation technology.
Beyond energy, the quality of the final product is vastly improved. In the paper industry, using the correct blade during chipper shredder blade replacement ensures that the fiber damage rate is minimized. For example, staggered bite designs in toothed blades help maintain the strength of recycled paper at levels ≥ 80 N m/g.
Finally, precision maintenance enhances safety and equipment longevity. By maintaining a strict clearance of 0.1-0.3mm between the rotating and fixed blades, operators avoid excessive extrusion, which prevents the blades from overheating and reduces the risk of catastrophic mechanical failure during high-speed operation.
Performance Metrics and Efficiency Gains
Quantifying the success of a chipper shredder blade replacement program involves tracking the "wear-resistant life" of the components. High-strength alloy steel blades made from Cr12MoV can reach a service life of 8,000 hours under continuous operation, provided that regular grinding and alignment checks are performed.
The integration of intelligent control systems further enhances these metrics. Systems that can detect a jam and automatically reverse the motor in less than 0.1 seconds significantly reduce the physical stress on the blades, extending the interval between replacements and reducing downtime.
Efficiency Comparison by Blade Material
Industrial Applications in Paper Recycling
In the realm of waste paper recovery, the cutter ring pulverizer is a critical component, rotating at speeds of 1500-3000rpm to grind boxes and newspapers into fiber flocs. For these machines, the timely chipper shredder blade replacement ensures a steady output of 0.08 to 1 ton per hour, which is vital for maintaining the production quotas of recycled pulp mills.
Furthermore, for the preparation of industrial-grade pulp, hammer mills equipped with alloy steel hammers (HRC55-58) are used to crush tough coated or straw papers. By maintaining a strict blade gap of 0.5-2mm in shredders, facilities can produce particles of 1-5mm, which are directly usable as raw materials, thereby increasing the overall material utilization rate to 98%.
Advanced Surface Strengthening Technologies
To push the boundaries of blade longevity, the industry has adopted surface strengthening techniques. Titanium Nitride (TiN) coatings are particularly effective, as they reduce the friction coefficient of the blade by 35%. This not only prevents the adhesion of paper scraps to the cutting edge but also slows the rate of abrasive wear, extending the time between each chipper shredder blade replacement.
Another breakthrough is the use of laser cladding technology. Instead of discarding a worn blade, laser cladding can be used to deposit new material onto the cutting edge, restoring the blade's service life to approximately 80% of its original new condition. This approach significantly reduces material waste and lowers the long-term cost of ownership.
When combined with paraffin lubrication for stainless steel blades or periodic coating repairs for carbide blades, these technologies ensure that the equipment remains operational under varied conditions—from the high-cleanliness requirements of medical paper processing to the rugged demands of urban solid waste centers.
Strategic Maintenance and Fault Prevention
Effective fault prevention begins with a rigorous inspection schedule. For alloy steel blades, edge wear should be checked every 8 hours of operation, while cemented carbide coatings require a comprehensive integrity check every 30 days. This proactive approach allows operators to schedule a chipper shredder blade replacement before a failure occurs, avoiding the risks associated with broken blades.
Lubrication is another overlooked but essential factor. Using specialized lubricants reduces friction and minimizes the probability of paper jams. When jams do occur, the response time of the intelligent overload protection system—typically under 0.1 seconds—is critical in preventing the blade from snapping under sudden torque spikes.
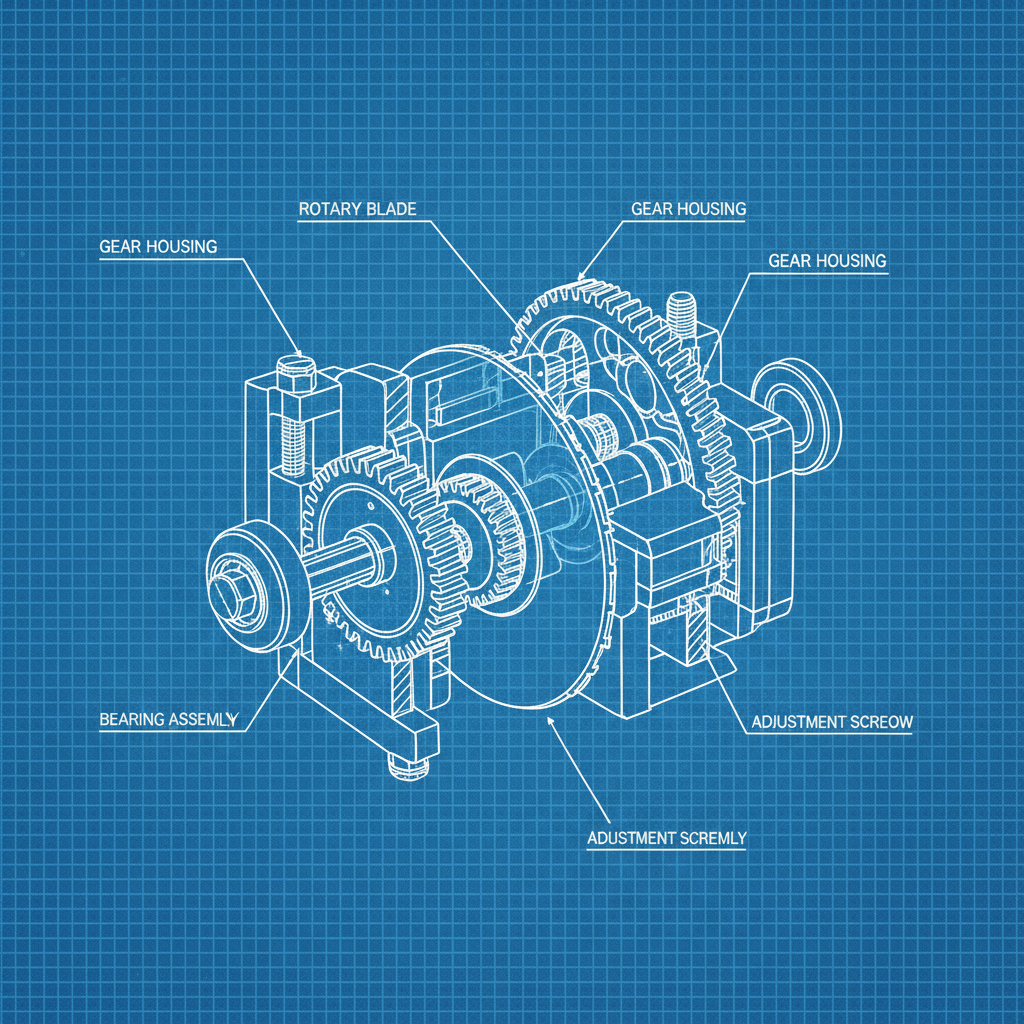
Finally, the adjustment of the clearance between the rotating blade and the static counter-blade must be meticulously controlled. Maintaining a gap of 0.1-0.3mm ensures a clean shear rather than a tear, which protects the blade edge from excessive extrusion and ensures that the energy is used for cutting rather than compressing the material.
Comparison of Blade Materials and Their Operational Suitability
| Material Type |
Primary Characteristic |
Ideal Application |
Durability Score (1-10) |
| Alloy Tool Steel (9CrSi) |
High Hardness / Low Cost |
Office Paper |
6 |
| Cold Work Die Steel |
Wear & Impact Resistance |
Cardboard/Laminated |
8 |
| Cemented Carbide |
Extreme Wear Resistance |
Metal Foil Composites |
10 |
| Stainless Steel |
High Corrosion Resistance |
Medical/Food Paper |
4 |
| TiN Coated Steel |
Low Friction Coefficient |
High-Volume Recyclables |
9 |
| Laser Clad Repair |
Restored Surface Integrity |
General Industrial Use |
7 |
FAQS
The frequency depends on the material being processed. For standard alloy steel blades in a paper recycling environment, you should check for edge wear every 8 hours. However, the actual replacement interval varies; cemented carbide blades can last significantly longer, but their coatings should be inspected every 30 days to ensure they aren't chipping or peeling.
For high-toughness materials like cardboard or laminated paper, Cold Working Die Steel (such as Cr12MoV or SKD-11) is the best choice. It provides a superior balance of wear resistance and impact resistance, preventing the blade from cracking while maintaining a sharp edge over a longer period compared to standard tool steel.
Yes, laser cladding technology is an excellent alternative to full replacement. This process allows for the additive repair of the cutting edge, restoring the blade's service life to approximately 80% of a new product. It is a cost-effective and sustainable way to manage wear in industrial shredding operations.
If the clearance exceeds 0.3mm, the machine will likely tear the material rather than cut it, leading to poor output quality and potential jams. If the clearance is too tight (below 0.1mm), it can cause excessive friction, overheating, and premature wear, necessitating an earlier chipper shredder blade replacement.
Titanium Nitride (TiN) coatings reduce the friction coefficient by 35%, which prevents paper scraps from adhering to the blade. This reduction in friction lowers the heat generated during the cutting process and significantly slows down abrasive wear, extending the overall operational lifespan of the blade.
Straight knives are best for low-confidentiality office paper and are cheaper to produce. Sawtooth knives, featuring serrated edges, are designed for high-toughness materials and high-security destruction. They offer lower cutting resistance on cardboard and make it nearly impossible to reconstruct the shredded documents.
Conclusion
Optimizing the shredding process requires a holistic approach that combines the right material science, precise geometric design, and a disciplined maintenance schedule. From the use of Cr12MoV steel for toughness to the application of TiN coatings for friction reduction, every technical choice impacts the frequency and cost of chipper shredder blade replacement. By focusing on precise clearance adjustments and adopting advanced repair technologies like laser cladding, industrial operators can maximize throughput while minimizing energy consumption and downtime.
Looking forward, the integration of intelligent control systems and frequency conversion technology will further refine the efficiency of waste processing. Investing in high-quality replacement components today ensures a sustainable and reliable production chain for the recycling industry. For those seeking professional-grade cutting solutions to enhance their operational efficiency, we invite you to explore our specialized range of industrial blades. Visit our website: www.bsblade.com