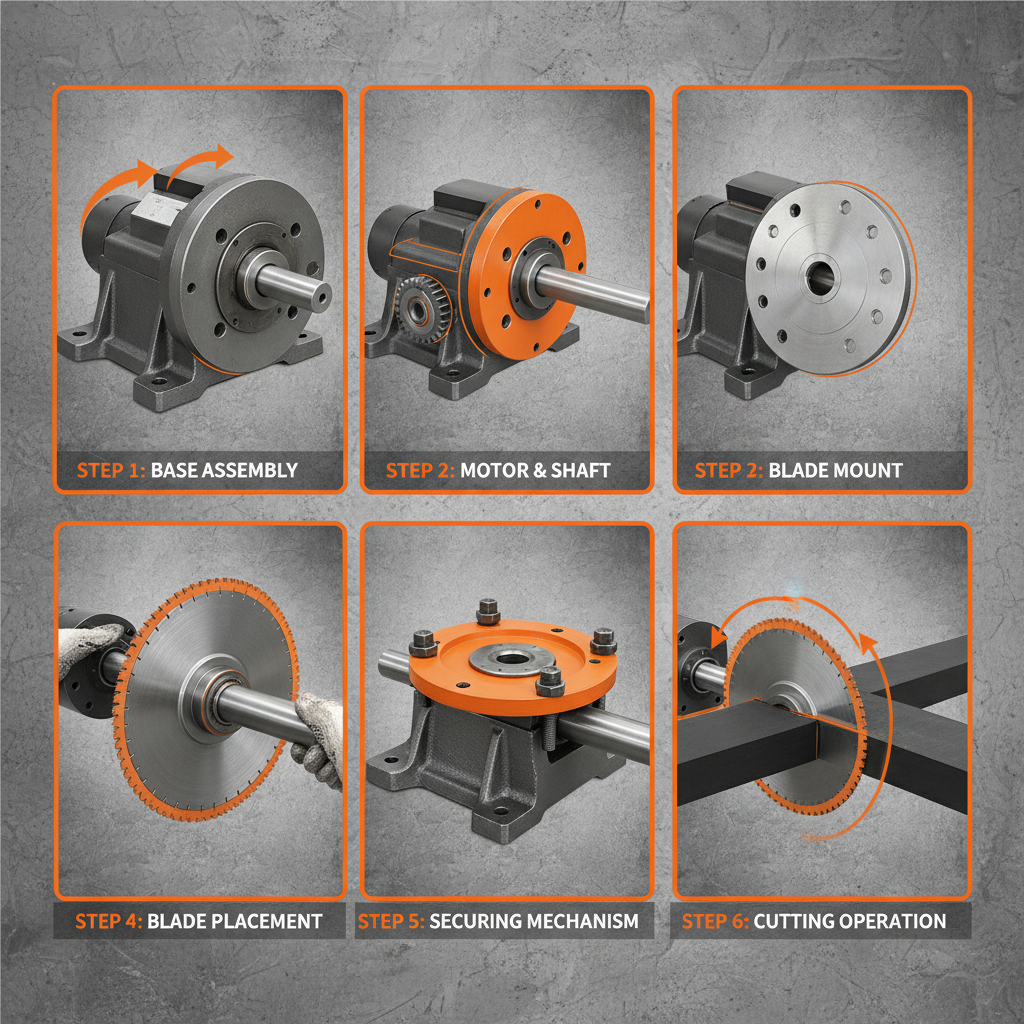
In the modern industrial landscape, the efficiency of material processing depends heavily on the quality of the cutting components used. High-performance cutting tools are essential for reducing downtime and maximizing the throughput of recycling centers and manufacturing plants worldwide.
The demand for robust shredding solutions has surged as industries shift toward circular economy models, emphasizing the recovery of valuable raw materials from waste streams. Achieving the perfect balance between hardness and toughness is the primary challenge in designing blades that can withstand extreme mechanical stress.
For operators looking to optimize their machinery, selecting the right wood shredder blades ensures a significant reduction in energy consumption and an increase in the purity of the final output material.
Global Industry Context of Wood Shredder Blades
Across the globe, the management of organic and industrial waste has become a critical priority for urban development and environmental protection. The integration of advanced shredding technology allows for the rapid transformation of bulky waste into manageable fragments, which is essential for biomass energy production and composting.
From the vast forestry sectors in North America to the urban waste management systems in Europe and Asia, the reliance on high-grade metallurgy in shredding equipment is evident. The challenge lies in creating tools that can handle inconsistent material density while maintaining a sharp cutting edge over hundreds of hours of continuous operation.
Defining the Technical Role of Shredder Blades
At its core, a shredder blade is a precision-engineered tool designed to apply concentrated shear force to a material, overcoming its structural integrity to break it into smaller, uniform pieces. These components are the "teeth" of the machine, and their geometry determines whether a material is sliced, torn, or crushed.
In the context of modern industry, these blades serve as the primary interface between the machine's power and the raw waste. Whether processing soft organic matter or high-density composites, the blade's ability to penetrate and shear without jamming is what defines the overall efficiency of the recycling line.
The connection to humanitarian and environmental needs is clear: by increasing the efficiency of shredding, cities can reduce landfill reliance and accelerate the creation of biofuels, contributing directly to global carbon reduction goals and sustainable resource management.
Core Material Components and Performance
The performance of wood shredder blades is fundamentally dictated by the metallurgy used during manufacturing. High-strength alloy steels are typically employed to ensure the blade can withstand the immense pressure of high-torque shredding without fracturing.
For demanding environments, the use of materials like Cr12MoV alloy steel, subjected to vacuum heat treatment, allows wood shredder blades to reach a hardness of HRC 58-62. This provides a critical balance of wear resistance and toughness, preventing the brittle fractures common in lower-grade steels.
Additionally, the application of specialized coatings such as Titanium Nitride (TiN) can significantly reduce friction. This not only extends the continuous operation life of wood shredder blades but also prevents the buildup of resinous materials that often cause clogging in organic waste processing.
Shape Classifications for Maximum Efficiency
Different materials require different cutting geometries to avoid machine overload. Straight edges are ideal for thinner, softer materials, providing a clean slice that minimizes energy draw. However, for tougher, more irregular waste, specialized geometries are required to "grab" and pull the material into the cutting chamber.
Curved or hook-shaped designs are often utilized to enhance penetration through hard objects, while serrated edges are employed to tear high-toughness materials. This prevents material jamming and ensures a consistent fragment size, which is vital for downstream processing in biomass plants.
Efficiency Comparison of Blade Geometries
Real-World Applications and Use Cases
In industrial forestry and landscaping, these blades are used to process massive volumes of branches, trunks, and root systems. By reducing these materials into a uniform mulch, companies can create high-value organic soil conditioners or feedstock for industrial boilers, reducing the cost of waste transport.
Beyond forestry, these tools are vital in the demolition and construction waste sector. When removing old wooden structures, high-strength blades allow for the separation of wood from nails and other metal contaminants, ensuring that the recycled wood can be safely repurposed without damaging future machinery.
Long-Term Value and Sustainability Benefits
Investing in premium grade cutting components yields tangible economic benefits. By reducing the frequency of blade replacements and sharpening cycles, operators can significantly lower their operational expenditure (OPEX) and increase the overall uptime of the production line.
From a sustainability perspective, the use of durable, long-lasting blades reduces the amount of scrap metal generated by the maintenance process itself. Furthermore, the increased efficiency in shredding leads to lower energy consumption per ton of material processed, reducing the carbon footprint of the recycling facility.
Ultimately, the reliability of these components builds trust in the recycling infrastructure. When a facility can guarantee consistent output quality and uptime, it attracts more waste-generating partners, accelerating the transition toward a zero-waste industrial ecosystem.
Maintenance Optimization and Future Trends
Effective maintenance is the key to prolonging the life of any cutting tool. Regular inspections for edge wear and the implementation of CNC-driven gap adjustment systems allow operators to maintain the optimal cutting angle, preventing the "rubbing" effect that leads to premature heating and material degradation.
Future innovations are moving toward "smart blades" integrated with wear-monitoring sensors. These sensors can alert operators in real-time when the blade thickness has worn beyond a specific threshold (e.g., 10%), enabling predictive maintenance that eliminates unexpected shutdowns.
Additionally, the shift toward additive manufacturing (3D printing with metal powders) is allowing for the creation of complex internal cooling channels within the blade. This could theoretically eliminate overheating during high-speed rotations, further extending the life of the tool.
Analysis of Blade Performance by Application Scenario
| Application Sector |
Recommended Material |
Optimal Blade Shape |
Durability Score (1-10) |
| Softwood Processing |
Alloy Tool Steel |
Straight Edge |
8 |
| Hardwood/Log Shredding |
Cr12MoV Steel |
Curved Hook |
9 |
| Construction Waste |
High Manganese Steel |
Serrated Tooth |
7 |
| Biomass Pelleting |
Tungsten Carbide Inserts |
Straight Edge |
10 |
| Industrial Pallet Recycling |
Cr12MoV + TiN Coating |
Composite |
9 |
| Urban Green Waste |
Standard Alloy Steel |
Curved Edge |
6 |
FAQS
The frequency depends on the material hardness and volume. For most industrial operations, a check every 200-300 hours of operation is recommended. If you notice an increase in energy consumption or a change in the output particle size, the blades should be ground immediately to maintain efficiency.
While technically possible, it is not efficient. Softwoods are best handled by straight-edged blades for clean cuts, whereas hardwoods and dense logs require curved or hook-shaped blades to prevent jamming. Using the wrong geometry can lead to excessive wear and possible motor overload.
Titanium Nitride (TiN) coating provides a very hard surface layer that reduces friction between the blade and the material. This prevents resin buildup from wood and significantly reduces abrasive wear, extending the interval between sharpening cycles.
Avoid pursuing maximum hardness (HRC) alone. Ensure the blades are made from a balanced alloy like Cr12MoV and have undergone a proper vacuum quenching and cryogenic treatment. This ensures that the blade possesses enough toughness to absorb shocks without brittle fracturing.
Carbide inserts offer extreme wear resistance and are ideal for highly abrasive materials. However, they are more brittle than solid alloy steel. For applications with potential contaminants like nails or stones, solid alloy steel with high toughness is generally a safer and more reliable choice.
The gap (clearance) between the rotating blade and the fixed counter-blade determines the shear efficiency. A gap that is too wide causes the material to fold rather than cut, leading to larger, irregular fragments and higher energy use. A gap of 0.1-0.5mm is typically optimal for most industrial shredders.
Conclusion
The selection and maintenance of high-quality shredding components are pivotal to the success of any material recovery operation. By aligning the metallurgical properties of the blades with the specific requirements of the material—balancing hardness, toughness, and geometry—operators can achieve a high-efficiency workflow that minimizes waste and maximizes resource recovery.
As we move toward an increasingly automated and green industrial future, the integration of smart monitoring and advanced coatings will continue to redefine the limits of durability. We encourage operators to move away from generic solutions and invest in precision-engineered tools to ensure long-term operational stability and sustainability. Visit our website: www.bsblade.com